 Rattan Export buyer guide: What Importers Should Check During A Rattan Factory Audit.
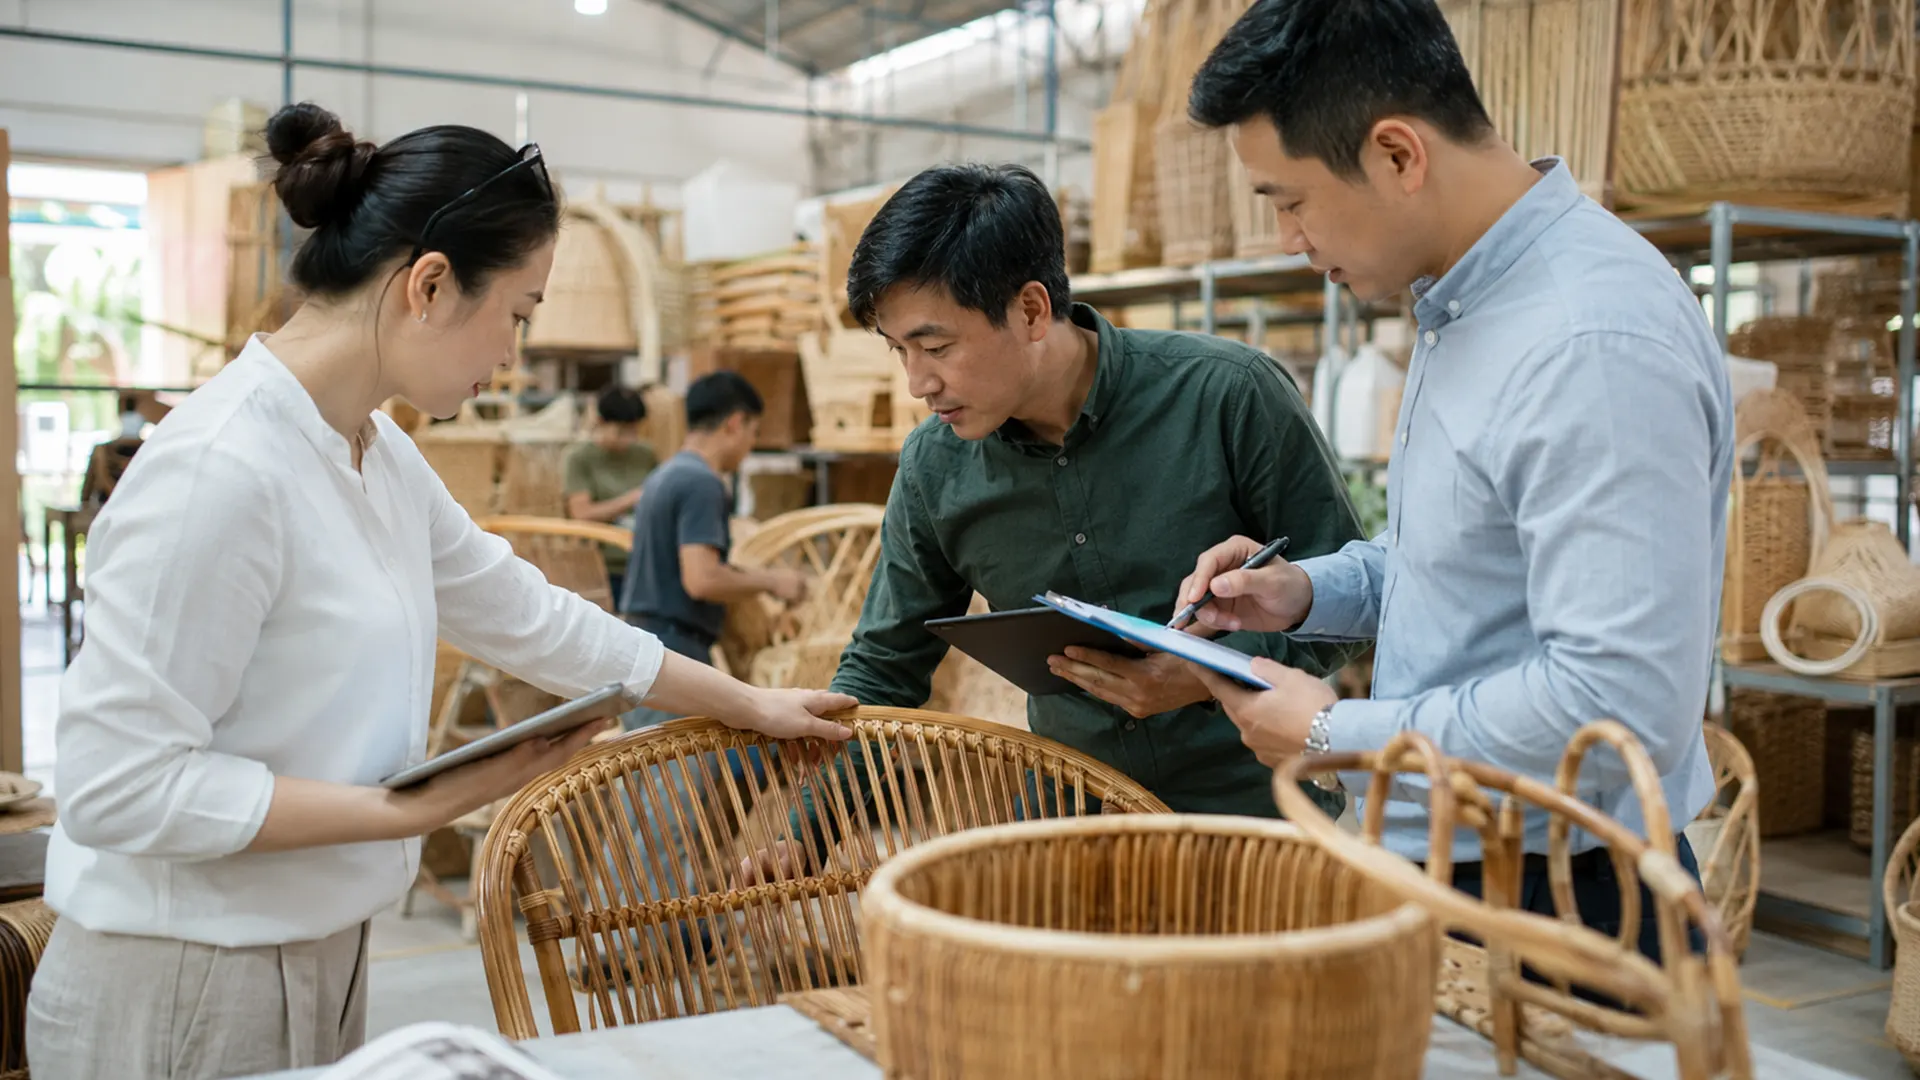
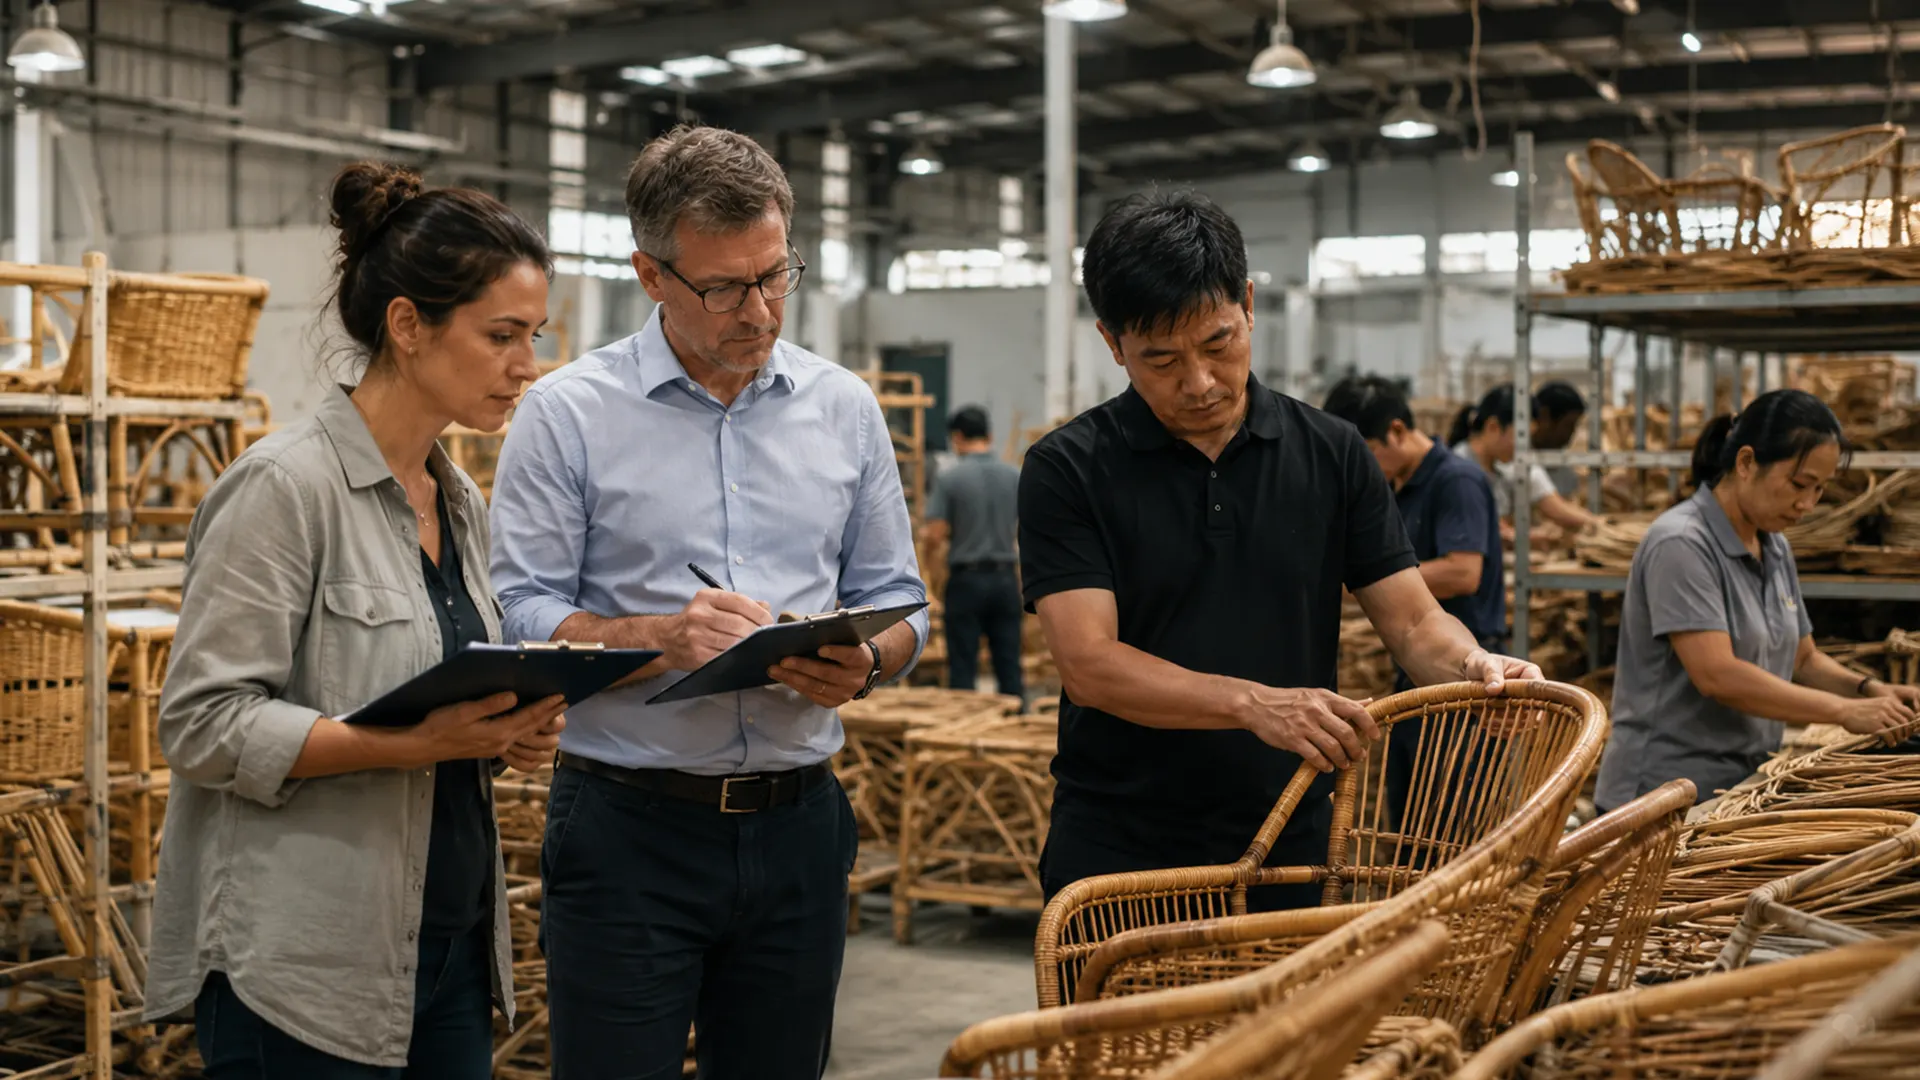
A rattan factory audit should verify much more than whether a supplier has attractive products, a clean showroom or a professional sales team. For international importers, wholesalers, distributors, retail chains, hospitality groups and project buyers, the purpose of an audit is to determine whether the factory can repeatedly convert approved specifications into export-ready products with controlled quality, realistic capacity, reliable lead times and disciplined packing and shipment procedures.
Rattan and bamboo production combines natural materials, manual craftsmanship, structural furniture construction, finishing processes and export logistics. That combination creates risks that may not be visible in a catalogue or sample room. A supplier can make an excellent development sample and still struggle with material consistency, moisture control, production repeatability, subcontracting, final inspection or container preparation during mass production.
A professional factory audit should therefore follow the real production flow—from incoming raw material to the finished carton—rather than focusing only on presentations prepared for visitors. Buyers sourcing within the Vietnam rattan, bamboo and natural-fibre manufacturing ecosystem should use the audit to understand what the factory actually controls, where risk enters the process and whether the supplier's systems are strong enough for long-term container-based purchasing.
1. Confirm That You Are Auditing The Correct Factory
Before evaluating production, confirm that the facility being visited is genuinely connected to the company that issued the quotation and will receive the order.
Check:
- Legal company name
- Factory name and address
- Relationship between sales office and factory
- Entity receiving payment
- Entity acting as exporter
- Whether production belongs to the company or a partner factory
A registered trading office and a production facility may be different legal entities. That is not automatically a problem, but the relationship should be clear before commercial commitments are made.
2. Do Not Audit Only The Showroom
Showrooms are useful for understanding design range, but they do not prove manufacturing capability.
A meaningful audit should include the actual:
- Raw-material storage area
- Material preparation area
- Cutting and bending stations
- Frame assembly area
- Weaving area
- Sanding and finishing area
- Upholstery area where applicable
- Work-in-progress storage
- Final quality-control area
- Packing area
- Finished-goods warehouse
- Container-loading area
The production observed should be reasonably consistent with the products the supplier is quoting.
3. Map The Entire Production Flow
Ask the factory to explain the production sequence for one representative SKU from beginning to end.
For example:
- Raw material received
- Material inspected and sorted
- Material conditioned or dried
- Components cut
- Rattan bent
- Frames assembled
- Joints reinforced
- Products woven
- Surfaces sanded
- Finish applied
- Finish cured
- Final assembly completed
- Quality inspection performed
- Product packed
- Cartons moved to finished-goods storage
- Container loaded
This reveals where quality gates exist and where uncontrolled movement between stages may create problems.
4. Identify Subcontracted Processes
Many furniture factories use subcontractors for selected processes. The important question is not whether subcontracting exists, but whether it is transparent and controlled.
Ask whether any of the following are performed outside the audited factory:
- Weaving
- Frame production
- Metal components
- Timber parts
- Upholstery
- Finishing
- Stone or glass components
- Packaging
If critical processes are subcontracted, determine how the factory controls specifications, incoming inspection, corrective actions and traceability.
5. Inspect Raw-Material Receiving
The quality of finished rattan furniture begins before production. A factory should have some method of checking incoming natural materials rather than accepting everything delivered by upstream suppliers.
Look for controls covering:
- Diameter
- Straightness
- Colour
- Surface condition
- Cracking
- Splitting
- Insect damage
- Contamination
- Moisture condition
Ask what happens to rejected material and whether acceptable and rejected stock are physically separated.
6. Check Material Storage Conditions
Raw rattan, bamboo and related natural materials should be protected from unnecessary moisture and contamination.
During the audit, observe:
- Whether material is stored directly on wet floors
- Whether rain can enter the storage area
- Whether airflow is reasonable
- Whether old and new material are mixed without control
- Whether visibly moldy material is segregated
- Whether materials are identified by type or batch where needed
Poor storage conditions can undermine later drying and quality-control efforts.
7. Audit Moisture-Control Procedures
Moisture management is one of the most important elements in natural-fibre furniture production. A factory audit should examine the process rather than searching for one universal moisture percentage.
Ask:
- At which production stages is moisture checked?
- Which components are measured?
- Which instruments are used?
- How are instruments maintained or calibrated?
- How are readings recorded?
- What action is taken when results are outside the agreed range?
- How long do products stabilize before packing?
One moisture-meter reading during an audit does not prove that the factory has a reliable moisture-management system.
8. Look For Mold Risk, Not Just Visible Mold
Visible mold is an obvious warning sign, but an audit should also identify conditions that can create mold later.
Warning indicators include:
- Persistent musty odor
- Wet floors
- Leaks
- Damp cartons
- Poor airflow
- Furniture packed immediately after wet finishing
- Finished goods stored in humid enclosed areas
- Contaminated rejected products mixed with acceptable products
Mold prevention should be integrated into the supplier's wider quality, moisture and pre-shipment control system.
9. Inspect The Bending Process
Rattan bending is a critical process because visual shape and structural integrity are created at the same time.
Audit points include:
- How material is prepared before bending
- Whether bending jigs or templates are used
- Consistency of radius and geometry
- Flattened or crushed fibres
- Hairline cracks
- Heat damage
- Asymmetry between left and right components
Repeated cracking in the same location can indicate a process or design issue rather than random natural variation.
10. Review Frame Assembly
Furniture frames should be evaluated for construction consistency, not only appearance.
Check:
- Joint fit
- Fastener position
- Reinforcement
- Frame symmetry
- Squareness where relevant
- Loose joints
- Excessive filler hiding poor joints
- Repeatability between units
Ask how the factory controls dimensions during frame construction.
11. Evaluate Weaving Workmanship
Hand weaving naturally creates some variation, but uncontrolled workmanship should not be confused with handcrafted character.
Inspect:
- Weaving tension
- Pattern consistency
- Spacing
- Loose ends
- Broken strands
- Edge finishing
- Bindings
- Excessive gaps
- Symmetry where the design requires it
Compare several production units rather than inspecting only one selected piece.
12. Check Whether Approved Samples Are Available On The Production Floor
Mass production should have an accessible reference standard.
The production team may need access to:
- Approved physical sample
- Technical drawing
- Dimensions and tolerances
- Material specification
- Approved weaving pattern
- Finish reference
- Hardware specification
- Packaging instructions
If only the sales department has the approved information, production errors become more likely.
13. Examine Finish Preparation
Many finish defects originate before stain or topcoat is applied.
Inspect:
- Sanding quality
- Dust removal
- Surface cleanliness
- Repair practices
- Preparation consistency
Poor preparation can cause uneven colour, rough surfaces, coating defects or visible repair marks.
14. Audit The Finishing Area
Finishing should be evaluated for both appearance and process discipline.
Look at:
- Colour-control method
- Approved finish samples
- Mixing or batch-control procedures
- Overspray control
- Drying area
- Curing time
- Protection from dust and contamination
- Ventilation and housekeeping
A surface being dry to the touch does not necessarily mean it is ready to be wrapped tightly for export.
15. Compare Several Finished Units For Colour Consistency
Natural materials will not be mechanically identical, but a production lot should remain within the buyer's approved visual range.
Do not rely only on digital photographs when establishing an important colour standard. Physical references can provide better control for repeated programs.
16. Check Dimensions During Production
Dimensional control should not be postponed until final inspection.
Ask:
- Which dimensions are considered critical?
- At which stages are they measured?
- What tolerances are applied?
- How are out-of-tolerance components handled?
For chairs and tables, small dimensional variation can affect stability, nesting, assembly and container efficiency.
17. Review Stability And Functional Checks
The factory should have appropriate checks for the intended product.
Examples include:
- Chair wobble
- Table stability
- Door alignment
- Drawer movement
- Hardware fit
- KD assembly
- Adjustable feet
- Moving components
Formal laboratory testing, where required, is separate from everyday factory functional checks.
18. Review Quality-Control Checkpoints
Ask where quality is checked during production rather than only asking whether the factory “has QC.”
A stronger system may include:
- Incoming-material inspection
- Frame inspection
- Post-weaving inspection
- Pre-finishing inspection
- Post-finishing inspection
- Final assembly inspection
- Pre-packing inspection
- Final random inspection
Not every product requires exactly the same checkpoints, but responsibilities should be defined.
19. Ask To See QC Records
Records provide useful evidence that a process exists beyond the day of the audit.
Possible records include:
- Incoming inspection reports
- Moisture readings
- In-process inspection sheets
- Final inspection reports
- Defect records
- Corrective-action reports
- Reinspection results
Records do not need to be complicated, but they should be usable and connected to real production.
20. Understand Defect Classification
Ask how the supplier distinguishes critical, major and minor defects where applicable.
Illustrative examples might include:
- Structural failure as a serious defect
- Missing hardware as a major usability defect
- Small cosmetic variation within an approved natural-material range as potentially acceptable
Actual classification should be agreed for the buyer's specific product and inspection standard.
21. Inspect The Rejected-Goods Area
A well-managed factory should have a clear method for handling failed products.
Check whether rejected items are:
- Clearly identified
- Separated from approved goods
- Reworked under control
- Reinspected before release
If rejected products can easily move back into acceptable inventory without authorization, the quality system is weak.
22. Review Corrective-Action Discipline
Ask for an example of a recent production problem and how it was resolved.
A meaningful corrective-action process should answer:
- What happened?
- Why did it happen?
- Which products were affected?
- What immediate correction was made?
- What process change prevents recurrence?
- How was effectiveness verified?
Repeated cosmetic repair without addressing root cause is not effective corrective action.
23. Verify Production Capacity Using Evidence
Do not accept capacity claims only as monthly container numbers.
During the audit, compare claims with:
- Available production space
- Number of workers
- Number of weaving stations
- Frame-production equipment
- Finishing capacity
- Current work in progress
- Current order backlog
- Packing capacity
Capacity should be evaluated for the buyer's actual SKU complexity.
24. Check Whether Capacity Depends On Temporary Outsourcing
A factory may quote high capacity by assuming large volumes will be transferred to outside workshops. This can be workable, but buyers should know it in advance.
Ask how outside capacity is qualified, inspected and traced.
25. Review Production Planning
Look for evidence that orders are scheduled rather than managed informally.
Useful planning information can include:
- Purchase-order number
- SKU
- Quantity
- Production stage
- Planned completion
- Inspection date
- Loading target
For mixed-container orders, synchronization across SKUs becomes especially important.
26. Check Traceability
Traceability does not need to resemble an automotive factory, but the supplier should be able to connect production with the relevant order, SKU and specification.
Where commercially necessary, records may also connect materials, finish batches, hardware or subcontracted components to a production lot.
27. Review Hardware Control
For KD furniture and mixed-material products, small components can create major claims.
Check:
- Hardware counting
- Bagging
- Identification
- Storage
- Protection from corrosion where relevant
- Placement inside the final carton
A missing low-cost bolt can make an expensive chair or table unusable.
28. Conduct A KD Assembly Check Where Relevant
If furniture is shipped knock-down, ask the factory to assemble a randomly selected packed unit using only the supplied hardware and instructions.
This can reveal:
- Misaligned holes
- Missing hardware
- Incorrect instructions
- Loose connections
- Part-identification problems
29. Inspect Upholstery And Cushions
Where furniture includes cushions or upholstery, review:
- Fabric identification
- Cutting consistency
- Stitching
- Foam specification
- Colour matching
- Cleanliness
- Storage conditions
- Protection during packing
30. Audit The Packing Area
Packaging should be treated as part of the product, not as a final warehouse activity.
Observe whether workers have clear instructions for:
- Surface wrapping
- Corner protection
- Leg protection
- Nesting separators
- Hardware placement
- Cushion placement
- Carton closing
- Carton labels
Different workers should not invent different packaging methods for the same SKU.
31. Measure Actual Final Cartons
Do not rely only on theoretical carton dimensions written in a quotation.
During a factory audit or packaging approval, measure the actual packed carton and confirm:
- Length
- Width
- Height
- Units per carton
- Gross weight
- CBM
These values affect landed cost and container planning directly.
32. Check Carton Strength And Stacking Logic
The outer carton should be suitable for the product's weight, size and expected stacking conditions.
Check whether stacking loads are transferred through structural areas rather than fragile woven panels.
Carton strength and packaging performance should form part of the buyer's broader inspection and approval system.
33. Inspect Finished-Goods Storage
Finished products may wait days or weeks before shipment. The warehouse should therefore be included in the audit.
Check:
- Dryness
- Cleanliness
- Airflow
- Rain protection
- Carton condition
- Separation of inspected and uninspected goods
- FIFO or other sensible stock rotation where relevant
Products that were dry when packed can still be exposed to poor conditions afterward.
34. Check Carton Marking And SKU Identification
Mixed-container and private-label programs require disciplined identification.
Cartons may need:
- SKU
- Product description
- Colour or finish
- PO number
- Quantity
- Carton number
- Barcode where applicable
- Handling marks
Physical cartons should reconcile with the final packing list.
35. Review Container-Loading Procedures
A strong factory audit should extend to the loading area when possible.
Ask how the factory controls:
- Container condition before loading
- Carton sequence
- Heavy versus crushable cartons
- Mixed-SKU positioning
- Unused gaps
- Final carton count
- Container number
- Seal number
- Loading photographs
Container-loading practices should connect with the broader export, freight and container-planning process.
36. Inspect Empty-Container Requirements
Before natural-fibre products are loaded, the factory or logistics team should check that the container is reasonably suitable.
Typical points include:
- Clean interior
- Dry floor
- No obvious water ingress
- No significant holes
- No strong abnormal odor
- Doors functioning correctly
A vessel cutoff should not be used as a reason to load a clearly unsuitable container.
37. Ask How Container Quantities Are Calculated
If the supplier states that a 40HC can load a certain number of chairs, ask for the calculation behind the claim.
Useful supporting information includes:
- Final carton dimensions
- Units per carton
- CBM per carton
- Loading layout
- Photos from previous comparable loads where available
Loading quantities should not be presented as universal standards.
38. Review Mixed-Container Capability
If your program combines chairs, tables, baskets, storage and decor, verify that the factory can manage multiple SKU priorities and carton types.
The loading plan should consider:
- Commercial priority
- CBM per SKU
- Carton strength
- Fragility
- Stackability
- Destination unloading sequence
39. Check Export Documentation Capability
Production quality is only one part of export execution.
Review responsibility for:
- Commercial invoice
- Packing list
- Shipping instructions
- Container and seal details
- Origin documentation where applicable
- Buyer-specific documents
Ask who prepares, checks and approves each document.
40. Review Previous Shipment Records Where Appropriate
Without requesting confidential customer information unnecessarily, previous shipment records can demonstrate whether the factory has real export routines.
Useful evidence may include anonymized packing lists, loading photographs, inspection records or internal shipment checklists.
41. Evaluate Housekeeping
Housekeeping may look like a cosmetic issue, but it often reveals production discipline.
Look for:
- Clear walkways
- Organized tools
- Controlled waste
- Separated chemicals
- Clean finishing areas
- Orderly storage
- Reduced cross-contamination risk
A factory does not need to look like a pharmaceutical laboratory, but uncontrolled clutter can increase damage, mix-ups and safety risks.
42. Review Basic Workplace Safety
Buyer audit requirements vary, but basic operational safety should not be ignored.
Observe:
- Emergency exits
- Fire extinguishers
- Electrical condition
- Ventilation in finishing areas
- Personal protective equipment where appropriate
- Safe chemical storage
- Machine guarding where relevant
Formal social-compliance audits may require a separate specialist assessment, but obvious safety concerns are still relevant to supplier risk.
43. Check Chemical And Finish Storage
Stains, coatings, solvents and adhesives should be stored in a controlled manner appropriate to the factory's processes.
Poor chemical control can affect:
- Product finish
- Worker safety
- Fire risk
- Batch consistency
- Contamination
44. Review Environmental And Social Requirements Relevant To Your Program
Different buyers and destination markets may impose different supplier requirements. These may involve material sourcing, waste handling, chemical management, labor practices or specific certifications.
Do not assume that a generic factory certificate automatically satisfies every buyer program. Scope and relevance should be verified.
45. Interview More Than The Salesperson
Useful conversations may include:
- Factory manager
- Production manager
- QC manager
- Warehouse supervisor
- Packing supervisor
- Export coordinator
Different answers to the same operational question can reveal whether procedures are actually standardized.
46. Compare Documents With Reality
An audit should test whether written procedures match actual practice.
For example:
- If records say moisture is checked, observe a real measurement.
- If cartons have a packing specification, watch one being packed.
- If rejected goods are segregated, inspect the rejection area.
- If production claims traceability, ask staff to trace one active SKU.
Documents are useful only when implemented.
47. Take Evidence-Based Audit Notes
Audit findings should distinguish between:
- Confirmed observation
- Supplier statement
- Documented evidence
- Open question
- Corrective action required
This makes follow-up more objective and prevents important issues from being lost in general impressions.
48. Classify Findings By Risk
Not every audit issue has the same commercial importance.
A practical classification might include:
- Critical: issue that could create major safety, legality or severe shipment risk
- Major: significant system weakness that can materially affect quality, delivery or commercial performance
- Minor: limited issue requiring correction but not indicating immediate systemic failure
- Observation: improvement opportunity that does not currently represent a failure
These categories are illustrative and should be adapted to the buyer's audit system.
49. Require A Corrective-Action Plan
An audit should not finish with a list of problems and no ownership.
For each significant finding, record:
- Finding
- Required correction
- Responsible person
- Target completion date
- Evidence required
- Need for follow-up verification
Major supplier-development value often comes from what happens after the audit.
50. Do Not Approve A Supplier Based On One Good Day
A factory audit provides a snapshot. Supplier approval should also consider:
- Sample performance
- Quotation accuracy
- Communication quality
- Trial-order performance
- Pre-shipment inspection results
- Packaging consistency
- Actual loading performance
- Claims and corrective actions
Long-term supplier confidence is earned through repeatable performance.
Practical Rattan Factory Audit Checklist
| Audit Area | What The Importer Should Verify |
|---|---|
| Company identity | Legal entity, factory location, exporter and payment beneficiary |
| Production scope | Internal production versus subcontracting |
| Raw materials | Receiving, grading, storage, moisture and rejection control |
| Bending | Cracks, crushing, geometry and process consistency |
| Frames | Joint quality, dimensions, reinforcement and stability |
| Weaving | Tension, pattern, bindings and workmanship consistency |
| Finishing | Surface preparation, colour control, curing and cleanliness |
| QC | Checkpoints, records, defects and corrective action |
| Capacity | Evidence supporting product-specific output claims |
| OEM/ODM | Ability to follow drawings, samples and technical changes |
| KD | Hardware control and assembly verification |
| Packaging | Protection, carton dimensions, CBM and repeatability |
| Warehouse | Dry, clean, controlled finished-goods storage |
| Loading | Container inspection, SKU control, carton count and seal records |
| Export | Documentation ownership and shipment coordination |
| Management system | Traceability, planning, housekeeping and communication |
Common Factory-Audit Red Flags
- The factory visited does not match the company quoting the order and the relationship is unclear
- The supplier refuses access to normal production areas without a credible reason
- Quoted products cannot be seen anywhere in production
- Natural materials are visibly wet, moldy or stored directly on damp floors
- There is no clear distinction between accepted and rejected material
- Repeated cracks are repaired cosmetically without process investigation
- Production staff do not have access to approved specifications
- Different workers pack the same SKU differently
- Finished cartons differ significantly from quoted dimensions
- QC records exist only as blank templates
- Rejected goods are not segregated
- Capacity claims are inconsistent with visible resources
- Subcontracting is hidden
- Bank, exporter or contracting entities change without clear explanation
- Container condition is not checked before loading
Positive Factory Indicators
- Transparent explanation of production scope
- Organized raw-material storage
- Clear production flow
- Accessible approved reference samples
- Visible in-process quality checkpoints
- Documented moisture monitoring
- Controlled rejection and rework areas
- Realistic production planning
- Consistent packaging instructions
- Accurate carton and CBM data
- Professional loading records
- Open discussion of current problems
- Evidence of corrective actions being closed
Frequently Asked Questions
How long should a rattan factory audit take?
There is no universal duration. A meaningful audit should allow enough time to inspect relevant production areas, review records, interview responsible staff and examine real products. Complex factories or broad product programs require more time than a simple specialist workshop.
Can a factory audit replace pre-shipment inspection?
No. A factory audit evaluates the supplier's systems and capabilities, while pre-shipment inspection evaluates a particular order. Both serve different purposes.
Should buyers announce audits in advance?
Many supplier audits are scheduled because responsible managers and records need to be available. However, buyers should still inspect normal production rather than only prepared demonstration areas.
Does a clean factory automatically mean good quality?
No. Cleanliness is positive, but buyers also need evidence of material control, technical capability, QC, process discipline and repeatability.
Is a small workshop automatically higher risk than a large factory?
No. A specialized smaller workshop may produce excellent products. The key issue is whether capacity, control systems and commercial expectations match the buyer's program.
Should subcontracting fail an audit?
Not automatically. The important questions are whether subcontracting is disclosed, controlled, traceable and subject to the buyer's specifications and inspection requirements.
What should happen after the audit?
Findings should be documented, significant issues assigned corrective actions and critical items verified before supplier approval or mass production.
A Factory Audit Should Test The System, Not The Presentation
The most useful rattan factory audits move beyond catalogues and prepared sample rooms. They test whether raw materials are controlled, production instructions reach workers, bending and weaving are repeatable, moisture risk is managed, defects are identified, corrective actions are implemented, packaging follows an approved method and the finished order can move reliably into an export container.
For international buyers, this is the real purpose of supplier auditing: not to find a factory that looks impressive for several hours, but to identify a production system capable of delivering consistent commercial results over many orders.
If you are evaluating a Vietnamese rattan or bamboo manufacturer for a 20ft, 40ft, 40HC, mixed-container, OEM, ODM, private-label or hospitality program, send your wholesale RFQ, product specifications, target quantities and supplier requirements so factory capability, quality controls, packaging and export readiness can be evaluated before the order is finalized.